

Crankshaft cutting

This site may earn a commission from merchant affiliate
links, including eBay, Amazon, Skimlinks, and others.

Joined
Sep 15, 2004
Threads
137
Messages
2,199
Location
Western Slope, CO
I'm currently under the spell of an engine rebuild for my 80. I selected a local shop to do the machine work, grind the crank, check and hone the block, cut the seats for the valves, clean, etc etc.

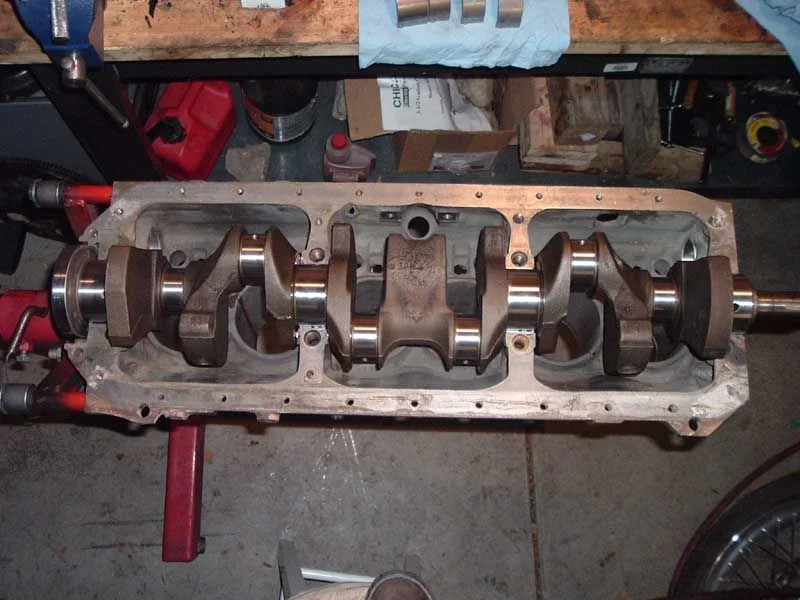
Everything was going okay for the reassembly of the lower half. Torqued down, the crack sets in the block and spins very smoothly, thrust clearance is slightly under nominal spec.

However, when I torqued down the conrods and try to turn the crack, nothing. The conrods are too tight.

I went back to the local shop and told him the predicament I was in. He said that with foreign motors the conversion factor from fractions to mm can cause problems. I assume that the crack grinding machine is not a modern machine with mm and factions built into it only fractions.

The crank was cut to accomadate .25mm undersized conrod bearings.
I'm taking the crack and rods back into the shop for a remeasure early next week.

Anyone run into a problem like this at a shop? If so, what was the solution(s).
DSCF0693mud.webp
 
Did you check the oil clearance with Plastigage?
 
Jim,

The inch to metric conversion line from your machinist is a crock. Use the Metric number multiplied x .03937 and you will get the inch number very accurately. Also I am sure there is a diameter tolerance plus/minus on the grinding spec that came with the bearings as a target. You may be closer than you think on this. torque the rod to spec with the bearings in it and take a bore guage to see the size of the bearing id. It may only need ground or polished .001 (1/5 of one of your hairs) to begin spinning. I am not a fan of plastigage but it works.

regards

Kirk
 
Find yourself a qualified machinist before this guy wrecks your crank! The oil clearances are critical. This is exactly the same problem I had when re-building my 3F. Was a nightmare to find a machine shop able to do a good job. Might be a good idea to get yourself plenty of plastigage and a micrometer, measure up the crank and inside rod bearing diameters - and tell the machinist exactly how much you want taken off.
 
Holy crap. The world of a machinist revolves around proper measurements and proper math. If the guy's excuse is a measurement problem, you're with the wrong guy. It's a little like a pilot crashing the plane you're on and afterwards giving the excuse that he had trouble with that whole "speed-lift-altitude thing" so it's not his fault.

The whole "metric/SAE thing" has been around for what - 90 years? And he still hasn't figured it out???!!

DougM
 
There is one other possibilty, and I throw it out there, not because I question anyones mechanical ability, but because I did this once myself. One of the bearings may have been installed backwards. And if that is the case, DO NOT TRY TO USE THAT BEARING! Once again, speaking from experience......
 
Wow, 3FE's only have 4 mains???
 
Are you sure you have the right rod bearings? maybe they gave you bearings for two undersizes of the crank. I'll speak in english terms because I don't know the metric comversions right off. maybe they cut the crank .010/.010 and you got .020 bearings
 
Dan,
No p.gage yet. I feel more confidence with a bore mic. But at this point in the rebuild, I think I'm going to try both just for reassurence.

Kirk,
Thanks for the edu. on the multiplier. That's what I was looking for. I'm planning on attending the re-measurement process with the owner of the shop for a second pair of eyes.

Edit: .:doh:the receprical of 25.4. Took me a little bit, but I got it.

Spike,
I'm confidence in the owners math ability. What I'm not confident in is the machines tolerence for slop. Meaning: The free play in the dial in between measurement mark X and measurement mark Y. I've seen this first hand at work with lathe work.

Doug,
I know. Which administration was it that decided to use a conversion factor instead of just going to metric. FORD.

toylndcrusr,
I'm doing the assemble myself. It's really hard to get the bearing backward's but I can understand how one might do this.


I'll keep ya'll posted.

Thanks again everyone:beer: :beer:
 
Last edited:
Back
Top Bottom